A deep navy that looks confident on a laptop screen can print noticeably brighter on an uncoated flyer. A warm beige packaging design can pick up a yellow cast under retail lighting. These are not small details when customers meet your brand through a menu, paper bag, banner or product box. This brand colour matching guide explains how to move from a digital brand palette to physical materials that look considered, consistent and recognisably yours.
Why brand colour changes between screen and print
Screens create colour with light. They use RGB – red, green and blue – and can display vivid, luminous shades that paper and ink cannot always reproduce. Commercial printing uses CMYK – cyan, magenta, yellow and black – where inks absorb and reflect light instead. The result is a different colour range, particularly for bright blues, greens, oranges and fluorescent-style shades.
That does not mean your printed materials will look wrong. It means colour needs to be specified for the final medium, rather than copied blindly from a website, presentation slide or social post. A strong brand system includes suitable values for both digital and print use, with clear guidance on where each should be applied.
The material also matters. A rich burgundy may look smooth and dense on a coated business card, softer on a textured letterhead and slightly different again on a kraft paper bag. Lighting, ink coverage, finishing and the printing method all influence the final impression.
Brand colour matching guide: start with the right values
Before approving artwork, identify which colour reference belongs to the job. RGB values are for digital displays. Hex codes are mainly used for websites and digital platforms. CMYK values are used for standard full-colour print. Pantone or spot colour references are pre-mixed ink standards used when colour accuracy is especially important.
For everyday brochures, flyers, catalogues and stickers, CMYK printing is often a practical and cost-effective choice. It produces excellent results for photographs and designs with several colours. However, a CMYK conversion may not precisely reproduce a highly saturated brand shade seen on screen.
If your brand relies on a signature colour, such as a distinct corporate blue, a specific red or a metallic tone, a Pantone spot colour can offer greater consistency across repeat print runs and product types. This can be particularly valuable for retail packaging, premium folders, event backdrops and high-volume campaign materials. It is not automatically necessary for every job, though. Spot colours can affect production cost and are best chosen when their benefit is clear.
Keep a simple record of your approved colour values. Your brand guide should ideally state the CMYK breakdown, RGB value, hex code and Pantone reference where relevant. Add rules for black, white and reversed-out versions of your logo too. This gives every designer, marketing team member and supplier a dependable starting point.
Convert early, not at the final approval stage
Designing in RGB and converting to CMYK just before printing can create surprises. A vibrant blue may become duller, while a bright green may shift towards olive. Build printed artwork in CMYK from the start when the primary output is physical, especially for large areas of solid colour.
Use the relevant CMYK profile for the print process where possible. Your print partner can advise on the suitable setup for the stock and production method. The aim is not to make colours look identical across every screen and surface. It is to make deliberate choices, then repeat them reliably.
Choose paper and materials as part of the colour decision
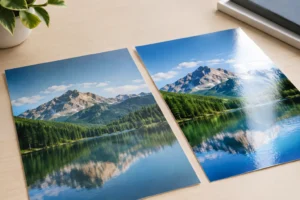
Paper is not a neutral backdrop. Its whiteness, texture and coating shape how your colours are perceived. Gloss-coated stocks tend to make photographs and saturated colours appear sharper and more intense. Matt-coated stocks reduce shine, creating a refined, contemporary look while still supporting good colour reproduction. Uncoated papers absorb more ink, often giving colours a softer, more natural finish.
For a finance firm, a crisp white uncoated letterhead may support a calm, trustworthy identity. For a beauty launch, a smooth matt box with a carefully chosen foil detail can make a restrained palette feel premium. A café using earthy colours may prefer kraft packaging because its natural base reinforces the brand story, but artwork must be adjusted for that darker substrate.
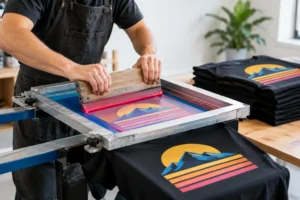
The same principle applies beyond paper. Fabric uniforms, acrylic signs, vinyl banners, corrugated cartons and stand-up pouches all receive colour differently. A colour that works on a menu may need a separate approved version for embroidered apparel or signage film. Consistency is about preserving brand recognition, not forcing one numerical value onto every production surface.
Be careful with large solid areas
Large blocks of dark colour are visually powerful, but they demand thoughtful preparation. A deep black background built from CMYK inks can show variation if the artwork, stock or finishing is not selected well. Your printer may recommend a rich black recipe for broad backgrounds, while small text usually needs a simple black value to remain sharp.
Likewise, very pale shades may disappear on uncoated stock, and fine white type reversed from a dark background can become difficult to read. Review contrast at the intended viewing distance. A striking design on screen still needs to work in a customer’s hand, on a shop shelf or across an event hall.
Use physical proofs for high-stakes work
A digital proof is useful for checking spelling, layout, image placement and general appearance. It cannot fully show how ink, paper and finishing will interact in the finished item. For packaging, major launches, corporate stationery systems, signage and repeat-order items, a physical proof or material sample is worth considering.
A proof lets you assess the colour in real conditions. Place it alongside existing branded materials. Look at it under daylight and the lighting where it will be used, such as warm restaurant lighting, office LEDs or retail spotlights. Check whether text remains legible, whether the logo holds its shape and whether the overall result feels like your brand.
It is also wise to approve a proof when using special finishes. Foil colours can vary in warmth and reflectivity. Spot UV creates contrast through shine rather than ink alone. Embossing and debossing introduce shadows that can change how a colour field appears. These techniques can create captivating works of art, but they should support the design rather than compete with it.
Build consistency across every customer touchpoint
Your brand is rarely encountered through one printed item. A customer may see a window decal, receive a promotional flyer, carry home a paper bag and later open a branded package. Each touchpoint can differ in size and material, yet the colour relationship should feel connected.
Start by prioritising the assets customers see most often. For many businesses, that means business cards, quotation folders, product labels, packaging, menus, point-of-sale displays and delivery inserts. Event organisers may focus first on backdrops, directional signs, badges and sponsor materials. Build these around the same approved palette, then adapt intelligently for their production requirements.
Avoid supplying a logo copied from a low-resolution web image or taking colours from a screenshot. Provide vector logo files where possible, along with the approved print colour references. Keep a master artwork folder with final versions clearly labelled by format and date. This saves time when teams need a quick reprint and reduces the risk of an old logo or incorrect shade returning to circulation.
For larger organisations, a short internal colour approval process can prevent expensive reworks. Decide who signs off on colour-sensitive materials, what must be proofed and which items can follow standard CMYK specifications. The process should be proportionate: a small run of internal forms does not need the same scrutiny as a nationwide product launch.
Common colour matching mistakes to avoid
The most frequent mistake is judging colour only from an uncalibrated screen. Another is assuming one CMYK build will look identical on every stock. Both can lead to disappointment, even when the artwork is technically correct.
Be cautious with designs that use very fine lines, tiny reversed text or subtle tonal differences. These details can be lost during printing, particularly on absorbent stock or at small sizes. Also remember that a finish can change perceived colour. Gloss lamination deepens and intensifies many colours, while matt lamination softens reflection and can make dark tones feel more elegant.
Finally, do not treat colour matching as a one-off task. When your business adds a new product line, changes packaging materials or plans an event, review how the palette will behave in that new setting. Good colour management protects recognition while giving your brand room to grow.
A dependable print partner should make these decisions easier, not more technical. Share your intended use, deadline, budget and existing brand references before production begins. With the right artwork, materials and proofing approach, 2B Printing can help turn your brand colours into polished physical materials that look at home wherever customers encounter them.